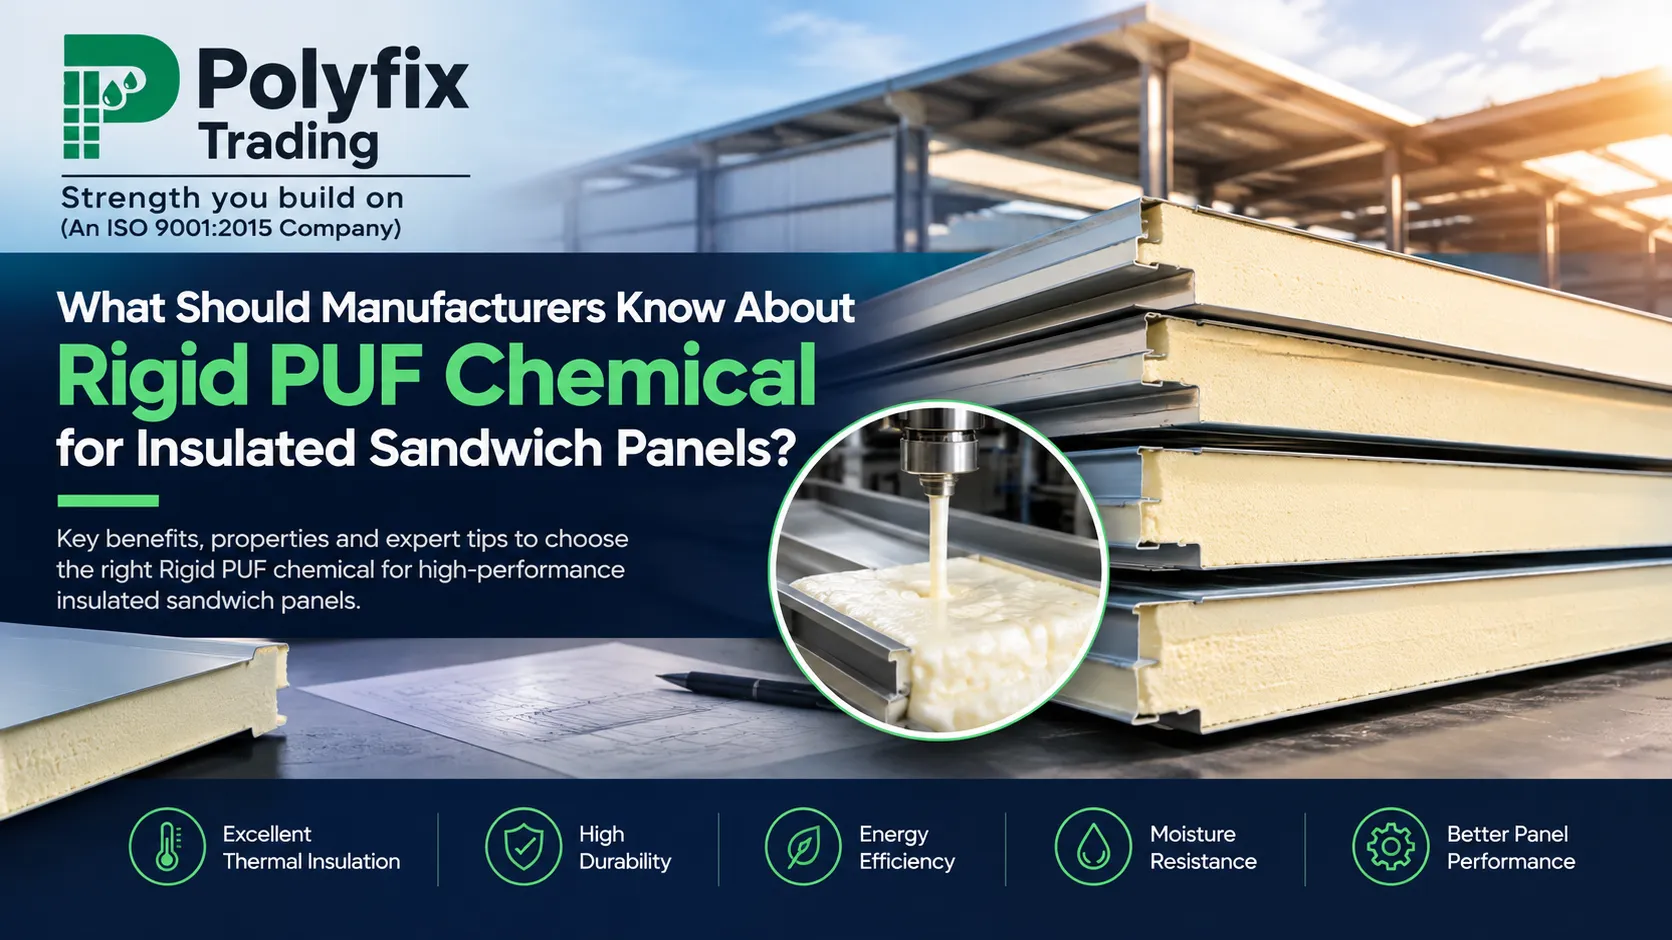
The chemical used in PUF sandwich panels is a two-component rigid polyurethane foam system: a Polyol blend and MDI (methylene diphenyl diisocyanate). Metered in the correct ratio and mixed in a mixing head, the two components react, expand, fill the cavity between two metal facings, and cure into a closed-cell rigid foam core that bonds to the facings as it sets. In India, panel cores are most commonly specified at a foam density of 40 ± 2 kg/m³, with panel thicknesses typically from 40 mm to 100 mm for general use and 60 mm to 150 mm for cold rooms. For a panel manufacturer, the chemical's flow, reactivity, adhesion, and batch-to-batch consistency matter as much as its thermal performance, because they decide whether every panel coming off your line is filled, bonded, and dimensionally stable.
If you run a panel line, or you're setting one up to serve cold storage, prefab, or industrial building demand around Hyderabad and Telangana, the foam core is the single most performance-critical material in your product. The metal facings give the panel its look and its stiffness, but the foam gives it its reason to exist: insulation. This guide explains how the chemistry works inside a panel, how the two common production methods place different demands on the chemical, what to check before you choose a system, and where Polyfix's Rigid PUF Chem RT-40 fits.
What Is PUF Panel Chemical?
Direct answer: PUF panel chemical is the liquid raw-material system, a Polyol component and an MDI component, that is injected or poured between two metal sheets to form the rigid polyurethane foam core of an insulated sandwich panel.
A finished sandwich panel has three layers: an outer metal facing (commonly pre-painted galvanised steel, PPGI, or galvalume, stainless steel, or aluminium), a rigid foam core, and an inner metal facing. Indian panel manufacturers commonly use facings around 0.4–0.5 mm thick, joined edge-to-edge with tongue-and-groove profiles and, for cold rooms, cam-lock fasteners embedded along the panel edges so panels pull tightly together on site.
"PUF panel chemical" is simply the trade name for what becomes the middle layer. It is not a ready-made foam; it is two reactive liquids that only become foam inside the panel, at the moment of manufacture. That is why chemical quality and process control are so closely tied together.
What Chemical Is Used in PUF Sandwich Panels?
Direct answer: PUF sandwich panels use a rigid polyurethane system made of Polyol and MDI, together with additives already formulated into the polyol side: catalysts, blowing agent, surfactant, and often a flame retardant.
Each part of the formulation has a job:
- Polyol (the resin side) carries the "recipe": catalysts that set reaction speed, a blowing agent that creates the gas that expands the foam, a surfactant that stabilises the cells as they form, and flame-retardant additives where fire performance is required.
- MDI (the isocyanate side) is the reactive partner. When it meets the polyol, the reaction generates heat and polymer, the blowing agent expands, and the mixture rises and gels.
- The ratio between the two is set by the formulation. Getting it wrong, even slightly, shows up as brittle foam, shrinkage, poor adhesion, or a core that never fully cures.
This is why Polyol and MDI should always be bought as a matched system whose ratio and behaviour have been validated together, not sourced separately from unrelated suppliers.
What Is Polyol + MDI in PUF Panels, and How Do They Create the Foam Core?
When Polyol and MDI are mixed, they undergo a chemical reaction that forms polyurethane polymer while the blowing agent expands the mixture into a foam. The foam rises, fills the cavity between the metal sheets, gels, and cures into a rigid closed-cell structure that adheres to both facings.
Panel manufacturers describe the process using four timing points, and every chemical system has its own values for them:
- Cream time: the moment the mixed liquid starts to turn creamy and begin reacting. The liquid should have levelled out in the cavity before this point.
- Rise time: the period during which the foam expands to fill the cavity. Rise should be complete before the foam starts to bond to the facings.
- Tack-free time: the point where the foam surface stops being sticky and begins adhering to the top facing.
- Mould release (demould) time: how long the panel must stay in the heated press or mould before it can be safely ejected without bowing or swelling.
This sequence is the heart of panel manufacturing. If foam starts gelling before the cavity is filled, you get voids and short fills. If it reacts too slowly, it can drain or leak, delay demould, and slow your output. A good panel system is one whose reactivity is matched to your machine, your panel length, and your mould temperature.
Continuous vs Discontinuous Production: Why It Changes What You Need from the Chemical
Direct answer: Continuous lines pour reacting foam onto a moving lower facing inside a double-belt press; discontinuous lines inject foam into a closed mould or press, one panel or batch at a time. The two methods place different demands on the chemical's flow, reactivity, and adhesion, so a system suited to one is not automatically right for the other.
| Factor | Continuous (double-belt) | Discontinuous (press / mould injection) |
|---|---|---|
| How foam is placed | Poured onto moving lower facing; foams and cures between belts | Injected through ports into a closed, often pre-heated mould |
| Typical scale | High volume, standard panel profiles | Small to medium volume, flexible sizes and profiles |
| What the chemical must do | Cure on a defined time-and-distance schedule; consistent output over long runs | Flow long distances inside a closed cavity before gelling; fill corners and edges fully |
| Common challenge | Consistency across long production runs | Voids, poor flow, and adhesion issues in closed-mould filling |
| Where it suits | Manufacturers with established volumes | Manufacturers making custom sizes, cold-room panels, or smaller batches |
Patent literature on discontinuous panel manufacture notes that closed-mould injection can suffer from poor flow and bonding if the chemistry is not well matched, and that vacuum-assisted injection is sometimes used to avoid voids and help homogeneous filling. Both processes typically use a high-pressure machine that meters the polyol and isocyanate accurately and mixes them in a mixing head. Raw materials are usually held in temperature-controlled tanks, often in the range of about 18–22 °C, because chemical temperature affects viscosity, mixing quality, and cell structure.
For a manufacturer, the takeaway is practical: tell your chemical supplier which process you run, at what mould temperature, and what panel dimensions you make. A supplier who cannot ask you those questions is not selecting a system for you; they are just quoting a price.
How Does Rigid PUF Improve Panel Insulation?
Rigid PUF improves panel insulation because its cells are predominantly closed and filled with low-conductivity gas, which limits heat transfer through the core; well-made rigid PUF typically achieves a thermal conductivity in the region of 0.021–0.026 W/m·K, better than most other panel core materials at the same thickness.
Three properties of the cured foam do the work:
- Closed-cell structure. Each tiny cell is sealed, which resists air movement and moisture, the two things that erode insulation performance over time.
- Low thermal conductivity. This is what allows a thinner PUF panel to match the insulation of a much thicker fibrous panel, saving wall thickness and usable interior space in cold rooms.
- Bond to the facings. A properly bonded core makes the panel behave as one structural unit, giving stiffness and load-bearing capacity well beyond what the foam or the sheets could offer separately.
Just as important is what the foam does not do well if the process is off. Voids, uneven density, or weak adhesion create thermal bridges and weak spots, which is why "good chemistry" and "good process" have to be evaluated together.
What Panel Density, Thickness and Application Should You Design For?
Indian panel manufacturers and suppliers widely quote 40 ± 2 kg/m³ foam density for PUF panels, with thickness options commonly running 40, 50, 60, 80 and 100 mm for general wall and roof panels, and thicker options up to 150 mm or beyond for cold rooms and freezers.
| Application | Typical Panel Thickness | What Matters Most |
|---|---|---|
| Prefab buildings, site offices, partitions | 40–60 mm | Cost, weight, ease of assembly |
| Industrial roofing and wall cladding | 40–100 mm | Thermal performance, panel stiffness |
| Chillers and cold rooms (above 0 °C) | 60–100 mm | Consistent insulation, tight joints |
| Freezer rooms (sub-zero) | 100–150 mm | Dimensional stability at low temperature, low thermal conductivity |
| Clean rooms and pharma enclosures | 50–100 mm | Surface finish, joint quality, hygiene |
Density is not a number to chase blindly. It is a balance: lower density saves chemical cost per panel but can reduce compressive strength and dimensional stability; higher density adds strength but also cost and weight. Whatever density you design to, the real test is whether the system holds it consistently across panels and across batches.
What Should Panel Manufacturers Check Before Choosing a Rigid PUF Chemical?
Check flow and fill behaviour in your mould or press, reactivity (cream, rise, tack-free, demould times) against your machine and panel size, adhesion to your chosen facing, dimensional stability after demould, batch-to-batch consistency, the supplier's technical support, and whether a trial quantity is available before bulk commitment.
Use this as a working checklist:
- Flow and fill. Does the system fill your longest panel completely, including edges and around cam-lock inserts, without voids or short shots?
- Reactivity matched to your line. Are cream, rise, tack-free and demould times documented, and do they fit your machine speed, mould temperature and panel length?
- Adhesion to facing. How does the foam bond to your specific facing (PPGI, galvalume, stainless, aluminium)? Manufacturers often improve bonding with surface treatments such as corona treatment on the steel, but chemical adhesion still matters.
- Dimensional stability. Do panels stay flat after demould and over time, or do they bow, swell or shrink?
- Density control. Can you hit and hold your target density with the metering ratio and pour weight you run?
- Fire performance requirement. Does your end use (cold storage for food and pharma, prefab, industrial) need a fire-retardant formulation, and can the supplier confirm the grade?
- Batch consistency. Will every drum behave like the last one? Ask about batch documentation.
- Storage and shelf life. MDI reacts with moisture; ask for clear storage guidance and shelf life.
- Technical support. Is there someone who understands panel lines and can help troubleshoot on your machine, or only a salesperson?
- Trial availability and GST invoicing. Can you test on your own equipment first, and will the supplier issue a proper GST invoice for input tax credit?
For a broader supplier-selection framework, see our buyer's checklist for rigid PUF chemical suppliers.
Common Panel Defects and What Usually Causes Them
Most panel defects trace back to a small set of causes. Use this as a diagnostic starting point when you speak to your chemical supplier.
| Defect | Commonly Points To |
|---|---|
| Voids or short fill, especially at edges | Insufficient shot weight, foam gelling before the cavity is filled, poor flow, or mould/raw-material temperature outside the intended range |
| Poor adhesion or delamination | Contaminated or untreated facing surface, cold facings, mismatched reactivity, or demoulding too early |
| Panel bowing or swelling after demould | Demould time too short, uneven mould temperature, or post-expansion of under-cured foam |
| Shrinkage of the core | Ratio or index issues, density too low for the design, or curing conditions outside range |
| Density variation panel to panel | Metering inaccuracy, temperature drift in the raw-material tanks, or inconsistent batches |
| Brittle or friable foam | Ratio imbalance or formulation mismatch |
The point is not to self-diagnose every defect from a table, but to show why process data and supplier support matter as much as the product itself. A chemical system that behaves predictably, and a supplier who can help interpret what your line is telling you, saves far more money than a few rupees off per kilogram.
Where Rigid PUF Chem RT-40 Fits
If you are evaluating rigid PUF systems for insulated panel and thermal insulation work, Rigid PUF Chem RT-40 from Polyfix Trading is one system worth including in your trials.
What it is: RT-40 is a two-component rigid polyurethane foam system supplied as a Polyol + MDI combination: a 20 kg matched pack made of 10 kg Polyol and 10 kg MDI. It is developed for refrigeration and thermal insulation applications, and forms a rigid, closed-cell foam structure intended to provide efficient thermal insulation, mechanical strength and dimensional stability.
| Specification | Detail |
|---|---|
| Product | Rigid PUF Chem RT-40, Polyol + MDI system |
| Product code / ID | RT-40 / PRD00161 |
| Pack | 20 kg (10 kg Polyol + 10 kg MDI) |
| Colour | Purple |
| Price | ₹275/kg (GST + transportation extra) |
| Coverage | Application and formulation dependent; technical guidance from Polyfix Trading |
Is RT-40 suitable for insulated applications? Yes. RT-40 is listed for refrigeration and thermal insulation use, including insulated sandwich panels, cold rooms and cold storage facilities, refrigerated trucks and reefer containers, and insulated doors.
An honest note on process fit. Every panel line is different, and no chemical supplier can tell you in advance exactly how a system will behave on your machine, at your mould temperature, in your panel sizes. That is exactly why RT-40 is supplied in a 20 kg matched pack: it lets you run a controlled trial on your own equipment, check fill, adhesion, demould behaviour and dimensional stability, and only then decide on larger volumes. Bulk drum quantities are available to discuss once your trial results are in. Continuous high-volume lines typically consume material in drum quantities, so we recommend discussing your line and volumes with our team up front.
Rigid PUF Chemical Supply for Panel Manufacturers in Hyderabad and Telangana
Telangana's growth in cold storage, food processing, pharma, warehousing and prefab construction keeps demand steady for insulated panels, and panel manufacturers in and around Hyderabad benefit from a local chemical supplier who can respond quickly when a batch needs attention. Polyfix Trading supplies PUF chemicals from New Bowenpally, Secunderabad, to panel makers, refrigeration manufacturers and contractors across Hyderabad, Secunderabad and wider Telangana, with technical guidance for grade selection and application.
For a wider view of our PUF range, grades and pricing, see our PUF chemical supplier guide for Hyderabad and Telangana. For how these panels perform once installed, see our cold storage insulation guide.
Frequently Asked Questions
What is PUF panel chemical?
PUF panel chemical is the two-component liquid system, a Polyol and MDI, that is injected or poured between two metal facings to form the rigid polyurethane foam core of an insulated sandwich panel. It is not a ready-made foam; it becomes foam through a reaction inside the panel during manufacture.
What chemical is used in PUF sandwich panels?
PUF sandwich panels use a rigid polyurethane system made of Polyol and MDI, with catalysts, blowing agent, surfactant and often flame retardant already formulated into the polyol side.
What is Polyol + MDI in PUF panels?
Polyol is the resin component that carries the additives which control reaction speed, foam cell structure and fire performance. MDI is the isocyanate component that reacts with the polyol to form polyurethane and drive foaming and curing. They must be used as a matched system in the specified ratio.
How does Polyol MDI create the foam core?
When mixed, Polyol and MDI react to form polyurethane polymer while the blowing agent expands the mixture. The foam rises to fill the cavity between the metal sheets, gels, and cures into a rigid closed-cell core that bonds to both facings.
How does rigid PUF improve panel insulation?
Rigid PUF has a predominantly closed-cell structure filled with low-conductivity gas, giving it low thermal conductivity, typically around 0.021–0.026 W/m·K. It also resists moisture and bonds to the facings, so the panel performs as a single insulated structural unit.
What should panel manufacturers check before choosing a system?
Check flow and fill in your mould or press, reactivity times against your machine, adhesion to your facing, dimensional stability, density control, fire performance, batch consistency, storage guidance, technical support, and whether a trial quantity is available.
Is RT-40 suitable for insulated applications?
Yes. RT-40 is a two-component Polyol + MDI rigid polyurethane system developed for refrigeration and thermal insulation applications, including insulated sandwich panels, cold rooms, refrigerated trucks and reefer containers, and insulated doors. Because process conditions differ from line to line, we recommend validating it with a trial on your own equipment.
Do you supply PUF panel chemical in Hyderabad and Telangana?
Yes. Polyfix Trading supplies rigid PUF chemical from Secunderabad to manufacturers and contractors across Hyderabad and Telangana, with technical guidance for application-specific questions.
Discuss Bulk PUF Chemical Requirements with Polyfix
If you are planning a trial, comparing systems for a new panel line, or need to discuss bulk quantities for an existing one, our team can help you match the system to your process rather than just quote a price.
Discuss bulk PUF chemical requirements with Polyfix →
📍 Polyfix Trading, 1-16-091, New Bowenpally Main Road, Opposite Delhi Mithai Bhandar, Secunderabad, Hyderabad, Telangana 500011
Related reading: Rigid PUF Chem RT-40